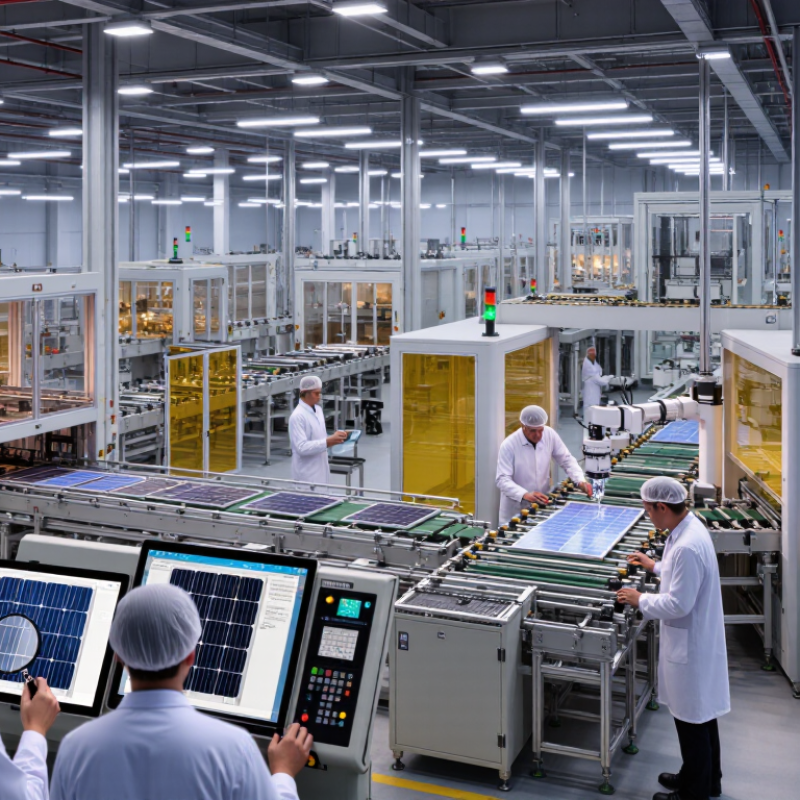
China Top PV Production Line How to Troubleshoot Errors?

Time:2026-10-11 Author:Sienna
0%

China’s PV manufacturing sector is expanding rapidly, but higher output also exposes hidden production-line weaknesses. The IEA PVPS Trends 2024 report recorded about 456 GW of new global photovoltaic capacity in 2023. Global cumulative capacity reached approximately 1.4 TW. Such scale makes stable factory performance essential.

This introduction explains How to troubleshoot PV production line errors through practical, traceable methods. Operators must inspect the complete process, including wafer handling, screen printing, cell sorting, tabber-stringer alignment, lamination, and final EL testing. A 0.2-millimeter soldering offset can create cell cracks that appear only after thermal cycling. A dirty camera lens can also produce false rejection alarms. Small clues matter.

NREL PV reliability researcher Dirk C. Jordan has emphasized, “A failure mechanism must be understood before a test can be trusted.” This principle applies directly to Chinese PV lines. Resetting an alarm may restore production, but it does not remove the cause. Engineers should compare machine logs, temperature curves, vacuum records, vision images, and defect maps. The ITRPV 2024 report also highlights increasing process complexity as advanced n-type technologies expand. That complexity demands tighter control and better evidence.

The process is rarely perfect. Sometimes, teams blame equipment too quickly. Sometimes, they overlook material variation. A reliable investigation should separate symptoms from causes, verify corrective actions, and record lessons for future shifts. This approach improves yield, safety, product consistency, and long-term customer confidence.

China Top PV Production Line How to Troubleshoot Errors?

PV Production Line Error Types and Their Root Causes

In China’s high-throughput PV factories, production-line errors usually appear before a complete shutdown. An alarm may indicate an electrical fault, but the real cause can be a loose connector or unstable power supply. Common electrical symptoms include overcurrent, voltage loss, sensor drift, and failed insulation checks. Record the alarm code, machine position, product batch, and exact time. Small details matter. This evidence prevents guesswork during maintenance.

Mechanical errors develop differently. Misaligned belts, worn bearings, blocked vacuum channels, and incorrect gripper pressure can damage wafers or cells. Fine glass dust may reduce suction, while poor calibration can create repeated cracks at one station. Thermal errors often involve uneven heating, blocked cooling, or inaccurate temperature sensors. Check actual readings with a calibrated handheld instrument. Do not trust the screen alone. Root causes may overlap.

Software and communication faults can stop material tracking, robot movement, or recipe selection. Network interruptions, outdated parameters, and permissive logic are frequent causes. Environmental conditions also matter: humidity, vibration, compressed-air quality, and airborne particles can change machine behavior. Experienced technicians isolate one variable at a time and restore settings from approved records. Replacing a sensor immediately feels efficient, but it can hide wiring damage. That shortcut deserves criticism. After repair, run a controlled trial and inspect the first output closely. A clean restart is not proof of a permanent fix.

How to Read Alarms and Verify Faults Safely

China Top PV Production Line: How to Troubleshoot Errors?

Modern PV lines demand disciplined alarm reading. The IEA PVPS Trends 2024 report estimates that global photovoltaic capacity exceeded 1.6 terawatts by the end of 2023. This scale increases pressure on equipment uptime and fault response. A red alarm is evidence, not a diagnosis. Record the alarm code, timestamp, machine state, recipe, and recent maintenance activity. Then check whether the alarm is active, latched, or historical. Read the sequence of events, not one message alone.

Keep people safe.

Before opening guards, isolate electrical, pneumatic, hydraulic, and thermal energy under the site procedure. Verify zero energy with approved instruments. Compare the alarm with physical evidence, such as a blocked film path, abnormal motor sound, vacuum loss, or a drifting temperature sensor. A second sensor, trend chart, or manual measurement can challenge a false reading. Never reset repeatedly. A rushed reset can hide a worsening fault. I have seen clean displays create false confidence. IRENA’s Renewable Capacity Statistics 2024 reports 2023 solar additions above 345 gigawatts, showing why repeatable verification matters across high-volume lines. Record the confirmed cause, failed check, corrective action, and restart result. If the evidence conflicts, stop and escalate to a qualified engineer.

China Top PV Production Line How to Troubleshoot Errors? - How to Read Alarms and Verify Faults Safely
System Area Typical Alarm or Symptom Likely Fault Safe Verification Method Typical Reference Data Corrective Action Risk Level
Production Line PLC Emergency Stop Active Emergency-stop button pressed, safety relay open, or safety circuit wiring interrupted. Check the HMI alarm history and inspect the emergency-stop circuit visually. Do not bypass the safety relay. Reset only after confirming that personnel and equipment are clear. Safety circuit should show a closed and healthy status after all emergency-stop devices are released. Identify the activated device, release it if safe, inspect connectors and safety relays, then perform a controlled reset. High
Glass Loading Glass Position Error Misaligned glass, failed photoelectric sensor, dirty reflector, or incorrect conveyor timing. Stop the line using the normal stop function. Inspect sensor lenses, glass position, guides, and conveyor movement. Apply lockout/tagout before reaching into the machine. Glass should remain within the equipment's specified positioning tolerance; the exact value depends on the line design and product format. Clean and align sensors, remove broken glass using approved tools, verify guide settings, and run a single-piece test. High
Cell Stringing Soldering Temperature Low Heater degradation, thermocouple fault, incorrect recipe, poor thermal contact, or insufficient warm-up time. Compare the controller reading with an independent calibrated temperature instrument. Perform verification only by trained personnel and follow the equipment's hot-surface controls. Typical soldering setpoints are commonly around 300–360 °C, but the approved value depends on ribbon, solder, flux, cell, and process qualification. Check the recipe, heater output, thermocouple connection, and warm-up time. Requalify the process after any temperature change. High
Cell Stringing Ribbon Soldering Open or Weak Joint Insufficient heat, excessive line speed, contaminated ribbon, poor flux application, or incorrect ribbon alignment. Inspect sample joints under magnification and compare pull-test or peel-test results with the approved process specification. Do not handle hot strings without thermal protection. Joint appearance should be continuous and free from visible voids, lifted ribbon, excessive solder balls, or cell cracks. Check solder profile, ribbon cleanliness, flux quantity, alignment, and pressure. Hold affected material until inspection is complete. High
Layup Station EVA or Encapsulant Misalignment Incorrect material width, roll tracking error, vacuum loss, feeder timing error, or product recipe mismatch. Verify the active recipe against the work order. Inspect web tracking and vacuum readings without placing hands inside the station. Encapsulant overlap and edge clearance must remain within the approved process specification for the module design. Correct the material roll position, repair leaks, verify feeder timing, and inspect the first articles after adjustment. Medium
Vacuum Laminator Vacuum Not Reached Door seal leakage, vacuum pump problem, clogged filter, valve failure, or trapped air path. Confirm the chamber is closed and guards are engaged. Review the pressure trend, inspect the door seal, and use an approved leak-test procedure. Many laminators operate with a vacuum setpoint near 0.5–2.0 kPa absolute, but the validated recipe is the controlling reference. Inspect seals and valves, clean or replace filters, check pump oil or pump condition, and repeat the leak test before production. High
Vacuum Laminator Lamination Temperature Deviation Heater-zone failure, inaccurate temperature sensor, airflow problem, or incorrect recipe selection. Compare displayed temperatures with a calibrated data logger or surface probe at designated test points. Avoid contact with hot surfaces. Common lamination recipes use approximately 140–160 °C, with cycle times often around 10–20 minutes; validated product parameters take priority. Check heater zones, sensors, recipe selection, and uniformity. Quarantine modules produced outside the validated process window. High
EL Inspection Dark Cell Area or Broken Cell Indication Cell crack, poor solder connection, inactive cell area, insufficient current injection, or camera exposure error. Confirm test current, exposure settings, and image focus. Use the approved electrical isolation procedure before opening the inspection enclosure. EL images should be compared with an approved reference library. Any electrically significant crack or inactive area requires engineering disposition. Separate the module, repeat the test, inspect solder joints and cell handling, and record the defect location for traceability. High
Framing and Curing Frame Adhesive or Sealant Incomplete Incorrect bead size, nozzle blockage, expired material, poor surface preparation, or insufficient curing time. Inspect bead continuity and width using a non-contact method where possible. Verify material batch, storage condition, and expiration date. Adhesive bead dimensions and curing time must follow the qualified process specification; incomplete coverage is not acceptable. Clean the nozzle, verify dispensing pressure and speed, replace unsuitable material, and repeat the inspection after curing. Medium
Junction Box Junction Box Bonding Failure Contaminated backsheet, insufficient adhesive, incorrect placement pressure, or bonding surface damage. Check position and coverage visually. Perform adhesion or pull testing only under the approved test method and after the specified cure time. Bonding strength and position must meet the qualified product specification; visual contact alone does not confirm bond strength. Improve surface cleaning, verify adhesive quantity and placement force, and hold modules until bond strength is confirmed. High
Electrical Test Insulation Resistance Low Moisture ingress, damaged cable, pinched insulation, contaminated surface, or junction-box sealing defect. Disconnect the module from all external circuits. Apply lockout/tagout, discharge capacitors, and use a properly rated insulation tester operated by qualified personnel. Acceptance limits depend on module rating and the applicable test standard; a commonly used screening value is above 40 MΩ·m², subject to the approved test method. Dry and clean the module, inspect cables and junction box, repeat the test, and reject or repair only according to the qualified procedure. High
Electrical Test Ground Continuity Failure Loose grounding connection, damaged frame path, oxidation, broken conductor, or incorrect test fixture contact. Verify test-fixture contact first, then use a low-resistance continuity tester with the module isolated from all live sources. Protective bonding resistance is normally required to be very low; the approved product specification and applicable safety standard determine the exact limit. Clean contact points, tighten or replace hardware, repair the bonding path, and repeat the test with recorded results. High
Flash or IV Testing Power Output Below Limit Cell mismatch, soldering defect, optical contamination, incorrect irradiance calibration, temperature error, or measurement instability. Verify irradiance, module temperature, reference device calibration, electrical connections, and test recipe before opening the module for investigation. Reference conditions are commonly 1,000 W/m² irradiance and 25 °C cell temperature. Output tolerance is defined by the product specification. Repeat the test after stabilizing conditions, compare the IV curve with known-good samples, and route persistent failures to process engineering. Medium
Conveyor and Servo Drive Servo Overload or Position Following Error Mechanical obstruction, excessive load, incorrect acceleration, coupling misalignment, or encoder feedback problem. Stop the equipment and isolate power before removing obstructions or accessing moving parts. Review drive diagnostics after the axis is in a safe state. Motor current should remain within the rated operating range; repeated peaks indicate a mechanical or tuning issue. Inspect bearings, belts, guides, couplings, and payload. Confirm motion parameters and perform a controlled homing sequence. High
Compressed Air System Low Air Pressure Compressor capacity problem, leaking tubing, closed valve, blocked filter, or excessive simultaneous demand. Read the pressure gauge from a safe location and inspect visible tubing. Depressurize the system before disconnecting pneumatic components. Many automated PV lines use approximately 0.5–0.7 MPa, but each machine's pneumatic specification is controlling. Repair leaks, replace clogged filters, open the correct supply valve, and verify pressure recovery under operating load. High
Traceability System Barcode or Serial Number Read Failure Dirty lens, damaged label, poor lighting, incorrect scanner focus, network interruption, or duplicate serial number. Check the scanner status and sample label without bypassing traceability controls. Confirm the serial number against the manufacturing execution record. Each finished module should have one unique, readable identifier linked to its process and test records. Clean the scanner, correct lighting or focus, reprint the label when authorized, and quarantine products with uncertain identity. Medium
Safety and Maintenance Repeated Alarm After Reset Intermittent sensor, loose terminal, failing actuator, software-state conflict, or an unresolved mechanical fault. Do not repeatedly reset the machine. Record the alarm code, timestamp, operating conditions, and preceding actions; then escalate to qualified maintenance personnel. Three or more repeated occurrences in one shift should normally trigger documented maintenance review, subject to site procedures. Analyze alarm history, inspect connections and components, test under controlled conditions, and document the verified root cause. High
Safety rule: Read the alarm before touching the equipment. Use the approved stop procedure, isolate all electrical, pneumatic, hydraulic, thermal, and stored-energy sources, apply lockout/tagout, verify zero energy, and allow only trained personnel to perform measurements or repairs. Reference values in this table are typical industry ranges; the approved equipment manual, product specification, process qualification, and applicable electrical and machinery safety standards always take priority.

Step-by-Step Troubleshooting for Mechanical and Electrical Issues

China Top PV Production Line: How to Troubleshoot Errors?

Step-by-Step Troubleshooting for Mechanical and Electrical Issues

When a PV production line stops, resist resetting it immediately. Record the alarm code, machine position, product condition, and recent maintenance work. A clear timeline often reveals the real trigger. Check guards, emergency stops, air pressure, and material alignment before opening any panel. Follow the site’s isolation procedure and verify zero energy with approved instruments.

Mechanical faults usually appear as noise, vibration, slipping, or uneven movement. Inspect rollers for contamination, worn bearings, loose fasteners, and incorrect belt tension. A misaligned conveyor can damage cells before the operator notices visible defects. Use a straightedge or laser alignment tool where available. Check pneumatic cylinders for leaks and confirm that grippers reach their full stroke. Do not force a moving assembly by hand.

Electrical troubleshooting requires measured evidence, not guesses. Inspect connectors, cable strain, sensor lenses, and cabinet ventilation. Compare supply voltage with the equipment specification, then test sensor signals at the terminal and controller. A missing signal may come from a damaged wire, poor grounding, or an incorrectly positioned target. Never bypass an interlock to keep production running. I have seen teams replace a sensor when the actual problem was a loose terminal. That mistake costs time. Recheck every assumption, document each test, and restart at low speed while watching temperature, current, and product quality.

China Top PV Production Line: Mechanical and Electrical Troubleshooting References

The chart shows common commissioning and troubleshooting reference values used on PV production equipment: three-phase AC supply, pneumatic pressure, protective grounding, insulation resistance, emergency-stop circuit continuity, and conveyor alignment tolerance. Always confirm the final limits against the machine manual, applicable electrical codes, and site safety procedures.

Testing, Repairing, and Restarting the Production Line

Troubleshooting a top PV production line starts with controlled testing, not guesswork. When an alarm appears, stop the affected section and record its code, time, product type, and recent adjustments. Check emergency stops, guards, air pressure, cooling flow, and electrical connections. Safety comes before speed.

Review the machine history before opening a panel. Inspect sensors for dust, loose cables, or misalignment. Use a calibrated multimeter only after confirming isolation procedures. A thermal camera can reveal an overheated terminal or motor. Compare readings with approved maintenance limits, not assumptions. Test one component at a time, then document every change. I have learned that the first diagnosis is not always right.

Replace damaged parts with verified specifications and tighten connections to the required torque. Clean optical surfaces carefully. After repair, run the line in manual mode at low speed. Check wafer handling, coating uniformity, temperature stability, vacuum levels, and alarm feedback. Restart production gradually, using a small batch for verification. Watch for abnormal noise, repeated alarms, edge cracks, or unstable output. A rushed restart is tempting. It can hide a deeper fault. If results remain inconsistent, stop again and involve qualified maintenance personnel. Keep the repair record, test values, photographs, and operator observations for future analysis.

Preventive Measures for Reliable PV Manufacturing

China Top PV Production Line How to Troubleshoot Errors?

Reliable photovoltaic manufacturing begins before alarms appear. The IEA PVPS Trends in Photovoltaic Applications 2024 reported over 1.6 terawatts of global installed PV capacity by the end of 2023. Such scale raises one question: can production lines remain stable under constant demand?

Preventive maintenance should follow equipment risk, not calendar habit. Inspect vacuum pressure, soldering temperature, conveyor alignment, and sensor drift every shift. Keep calibration records with actual readings, not simple “pass” marks. A 0.5°C temperature deviation may alter solder quality across thousands of cells. IEC 61215 and IEC 61730 testing principles also support stricter process controls. Short checks matter.

When an error appears, operators should preserve the alarm code, product batch, and recent parameter changes. Restarting immediately can erase useful evidence. IEA PVPS data shows that reliability increasingly depends on quality management, not capacity alone. NREL field research has reported typical module degradation near 0.5% annually, but manufacturing defects can accelerate losses. Our own line reviews sometimes reveal an uncomfortable weakness: preventive checklists are completed, yet abnormal noise goes unreported. Training must include sound, vibration, and visual changes. Human judgment remains imperfect. That is precisely why layered inspections, spare sensors, and documented root-cause reviews are necessary.

FAQS

What should operators do when a PV production line stops?

Record the alarm code, machine position, product condition, and recent maintenance work. Do not reset immediately. This timeline may reveal the trigger.

What safety checks should happen before opening a machine panel?

Check guards, emergency stops, air pressure, and material alignment. Follow the site isolation procedure. Verify zero energy with approved instruments.

How can operators identify a mechanical fault?

Look for unusual noise, vibration, slipping, or uneven movement. Inspect rollers, bearings, fasteners, and belt tension. A small rattle can become costly.

How should conveyor alignment problems be checked?

Use a straightedge or laser alignment tool when available. Check whether rollers run evenly. Misalignment can damage cells before defects become visible.

What should operators inspect on pneumatic components?

Check cylinders for air leaks. Confirm grippers complete their full stroke. Never force a moving assembly by hand.

What evidence is useful during electrical troubleshooting?

Inspect connectors, cable strain, sensor lenses, and cabinet ventilation. Compare supply voltage with equipment specifications. Test sensor signals at the terminal and controller.

Why might a sensor fail to send a signal?

Possible causes include damaged wires, poor grounding, or a misplaced target. A loose terminal can imitate a failed sensor. I have seen teams replace the wrong part.

Should operators bypass an interlock during production?

No. Never bypass an interlock to maintain output. Use the approved isolation and repair process. Safety must outweigh short-term production pressure.

Which preventive checks support stable PV manufacturing?

Inspect vacuum pressure, soldering temperature, conveyor alignment, and sensor drift every shift. Record actual measurements, not only “pass.”

How can teams improve root-cause analysis after an error?

Preserve the alarm code, product batch, and recent parameter changes. Restart at low speed after repairs. Watch temperature, current, and product quality. Checklists help, but they are not perfect.

Conclusion

This guide explains How to troubleshoot PV production line errors by identifying common fault types and tracing their root causes. It covers mechanical problems such as misalignment, material jams, vibration, and worn components, as well as electrical and control issues involving sensors, wiring, power supplies, communication, and software alarms. Operators will learn how to read alarm messages, confirm symptoms safely, and distinguish between the reported fault and its actual source before taking corrective action.

The article also presents a practical process for isolating problems, testing components, repairing or replacing damaged parts, and restarting the line in a controlled manner. Safety checks, recordkeeping, trial runs, and performance verification are emphasized to reduce downtime and prevent repeated failures. Finally, it outlines preventive measures, including routine inspections, equipment cleaning, calibration, staff training, and maintenance planning, helping PV manufacturers improve reliability, product consistency, and long-term production efficiency.

Sienna

Sienna

Sienna is a skilled marketing professional with a deep expertise in our company’s core products and services. With a passion for innovation and detail, she plays a pivotal role in crafting insightful blog posts that not only highlight the unique features of our offerings but also provide valuable......